Cheese Cutting Hygiene: Cleaning Access and Process Validation
Hygiene is a core consideration when selecting equipment for cheese processing. Cutting blades, product supports, conveyors, guards, and nearby contact surfaces may encounter food residue during production. The way these parts are accessed, cleaned, inspected, and returned to service influences the practicality of a cutting system.
Ultrasonic cheese cutting may offer process benefits for selected products, but it does not remove the need for established sanitation procedures. Manufacturers should evaluate cleaning access and residue behavior as carefully as cut quality, portion consistency, and line integration.
Where Cleaning Challenges Can Occur
Blade and Product-Contact Surfaces
Cheese may leave residue on a blade, particularly when the product is sticky, soft, warm, or prone to smearing. Other product-contact surfaces can collect fragments or crumbs. The level and type of residue vary with cheese formulation, temperature, cutting geometry, and the number of consecutive cuts.
During equipment evaluation, identify all surfaces that contact product or may be exposed to splash, fragments, or residue. Review whether operators can inspect these areas and follow the cleaning method specified by the equipment manufacturer.
Conveyors, Guides, and Transfer Points
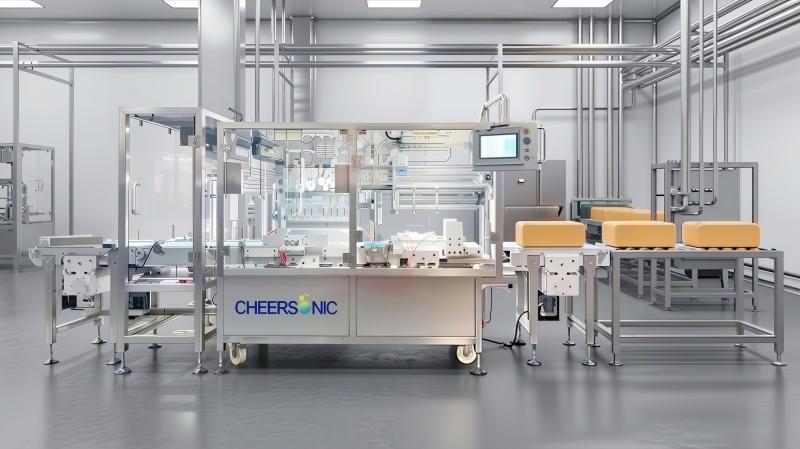
Product handling components may also need attention. Cheese pieces can collect around guides, transfer points, fixtures, and conveyor edges. A cutting station that produces a good cut but is difficult to clean may create operational burdens during changeovers or sanitation stops.
Recipe Changes and Product Variety
When several cheese varieties are processed on one line, residue characteristics and cleaning needs may change between recipes. A cleaning plan should account for the actual product sequence, equipment design, and the processor’s food-safety procedures.
Does Ultrasonic Cutting Change Cleaning Needs?
Ultrasonic cutting systems use a generator and transducer to create high-frequency vibration in a purpose-designed blade. In suitable applications, the vibration may reduce cutting resistance and help limit dragging or material adhesion. Some cheese trials may therefore show a difference in blade residue compared with conventional cutting.
However, residue reduction is product-specific and should not be treated as proof that a cleaning step can be skipped. Sanitation requirements depend on the food-safety program, equipment design, applicable rules, and the manufacturer’s validated procedures. The equipment selection process should separate cutting-performance claims from hygiene validation.
How to Evaluate Cleaning Access
Include cleaning and inspection in the sample-test plan. Ask the equipment supplier to explain the approved cleaning method, the parts that can be removed, and any restrictions on water or cleaning agents. Do not apply a cleaning method that conflicts with the manufacturer’s instructions.
- Access: confirm that operators can reach relevant food-contact areas for inspection and cleaning.
- Residue points: identify places where cheese fragments or smears accumulate.
- Disassembly: understand which parts may be removed and how they are reinstalled safely.
- Cleaning procedure: document the approved process and required tools or agents.
- Verification: follow the processor’s approved method for confirming that cleaning is complete.
- Restart: define the inspection and safe restart steps after cleaning or maintenance.
Record Residue and Cut Quality Together
Residue should not be assessed in isolation. If material accumulates on a blade, inspect whether the cut surface, dimensions, or product handling also changes. A structured trial can record the number of cuts, product temperature, residue observations, cleaning interval, and any quality defects.
Ultrasonic cutting may be compared with the current method using the same cheese and comparable conditions. If the trial includes different formulations, record each one separately. A single favorable sample does not establish performance across every product.
Integrating Hygiene With Intelligent Cutting
An intelligent cheese cutting system may combine ultrasonic cutting with 3D scanning, AI computing, and weighing functions, depending on configuration. These features may support measurement, recipe selection, and portion checks, but they do not replace sanitation design or validation.
Review how the system fits the facility’s cleaning workflow, including operator access, guarding, control interfaces, conveyor layout, and changeovers. Ensure that automation does not make inspection or safe cleaning more difficult.
Discuss Your Requirements With Cheersonic
Cheersonic supports food manufacturers evaluating ultrasonic food-cutting applications. Visit the Intelligent Cheese Cutting System page as a starting point for discussing product handling and equipment configuration.
Contact Cheersonic with your cheese type, production sequence, residue concerns, and sanitation requirements. Qualified manufacturers can arrange a sample cutting test to assess cut quality and residue while reviewing how the equipment may fit the intended process.
Frequently Asked Questions
Does ultrasonic cutting eliminate sanitation requirements?
No. Cleaning and sanitation must follow the processor’s approved procedures and equipment instructions.
Can reduced blade residue prove that equipment is hygienic?
No. Visible residue and sanitation verification are different matters. Follow validated food-safety procedures.
What should be checked before buying equipment?
Review food-contact access, cleaning instructions, disassembly, residue points, maintenance, and safe restart procedures.
Should each cheese variety be tested?
When products have different formulations or cutting behavior, evaluate them separately or use a documented, representative validation plan.
Email: market2@cheersonic.com
WhatsApp: +8615869049660